Combustible Dust: A Hidden Hazard That Demands Reliable Dust Collection
Key Highlights
- Effective dust collection is critical to preventing combustible dust accumulation and reducing fire and explosion risk.
- Poor valve performance increases energy consumption, maintenance requirements, downtime risk, and operating costs.
- SMC's SMARTVENT® dust collection system reduces compressed air waste while improving reliability and service life.
Dust is an unavoidable byproduct of many food processing operations. Milling, conveying, mixing, grinding, and packaging ingredients such as grain, sugar, flour, cocoa, and cornstarch routinely generate airborne particulate that must be captured and controlled. While dust collection systems are commonly viewed as environmental or housekeeping equipment, their role extends far beyond cleanliness; they are required to mitigate fire and explosion hazards.
When combustible dust accumulates in a manufacturing environment, the consequences can be severe. Fine dust particles that appear harmless during normal production can become a significant hazard when suspended in the air. If a combustible dust cloud meets an ignition source, the resulting combustion event can escalate rapidly, causing fires, explosions, equipment damage, and potential risk to employees.
The challenge for manufacturers is that effective dust collection depends on more than simply installing a collection system. Performance consistency is critical. Filters must be maintained, dust accumulation must be controlled, and cleaning cycles must operate effectively to prevent the buildup of combustible particulate.
At the center of many industrial dust collection systems is the reverse pulse jet valve. These valves deliver short bursts of compressed air that create the pressure wave necessary to remove dust buildup from filter elements. When these valves perform correctly, they help maintain filtration efficiency and support continuous operation. When valve performance declines, the consequences can extend beyond reduced cleaning efficiency.
Poor-performing valves can create a chain reaction of operational issues:
- Filters may not clean effectively, allowing dust loading to increase.
- Systems may require more frequent cleaning cycles, increasing compressed air consumption.
- Production teams may experience more frequent maintenance interventions and diaphragm replacements.
- Reduced dust collector performance can increase operational risk and downtime exposure.
The importance of reliable valve performance becomes even greater as manufacturers increase production demands and operate increasingly complex processes. A dust collector that is technically installed but not operating efficiently can create a false sense of protection. Safety depends not only on having a collection system in place, but on ensuring that system continues to perform as designed throughout its operating life.
Compressed air consumption is another overlooked factor. Many legacy reverse pulse jet valves may continue releasing compressed air longer than necessary after the required cleaning pulse has already been delivered. This wasted air represents unnecessary energy consumption while providing limited additional cleaning benefits. Across a facility running hundreds of valves, that inefficiency adds up: a manufacturer operating 200 dust collectors can lose more than 5 million kilowatt-hours a year to wasted compressed air alone, over $500,000 in annual cost.
Maintenance practices also influence long-term reliability. Many legacy valve designs rely on replaceable diaphragms and repair kits as part of normal operation. Most valve makers are confident their valve will fail, they cast the words REPAIR KIT into the valve itself, along with the repair kit number so it’s easy for the end user to keep ordering them. While repair programs may restore functionality temporarily, repeated component replacements introduce additional labor requirements, maintenance planning challenges, and potential production interruptions.
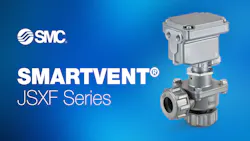
Valve design has a direct, measurable effect on all three of these cost drivers. SMC’s JSXF Series, the valve behind the SMARTVENT® dust collector system, is engineered to close immediately once the sonic shockwave needed for filter cleaning has been delivered, rather than continuing to bleed air afterward. Since SMC’s introduction to the U.S. market in 2017, the JSXF series has recorded zero valve failures and is rated for a lifecycle of 10 million lifecycles at 130 psi.
At the core of the system is a simple and robust design featuring a heavy elastomer diaphragm, no springs, and the SMARTVENT® solenoid valve mounted directly above the diaphragm. This design minimizes wear-prone components while maximizing reliability and service life.
The modern manufacturing environment requires a different approach; one that considers dust collection performance, energy efficiency, lifecycle reliability, and total cost of ownership together. A dust collector should not simply function as a reactive piece of equipment requiring frequent intervention; it should operate as a reliable production asset supporting both safety and operational goals.
This is where advancements in reverse pulse jet valve technology become increasingly important. By improving pulse delivery, reducing unnecessary compressed air consumption, and extending component life, modern valve designs can help manufacturers move beyond reactive maintenance strategies and toward more predictable, reliable dust collection performance.
Effective combustible dust management begins with recognizing that a dust collection systems is not a passive safeguard. They are active safety and production systems that require reliable performance at every operating cycle.
For manufacturers seeking to strengthen dust collection reliability while cutting energy and maintenance costs, the next step is evaluating whether the technology inside the system is helping achieve these goals or creating additional risk.
To explore how advanced reverse pulse jet valve technology addresses these challenges, read “SMARTVENT® Dust Collector Valves Reduce Compressed Air Consumption up to 62% and eliminate the ‘Repair Kit Trap’ Costing up to $4,428.57 per Hour,” which examines how engineering improvements in valve design can reduce compressed air waste, extend service life, and improve dust collector performance.